Air Compressor CFM vs PSI Chart Guide for Motor Longevity
This post contains affiliate links. As an Amazon Associate, we earn from qualifying purchases.
An air compressor CFM vs PSI chart shows an inverse relationship: as pressure (PSI) increases, the volume of air delivered (CFM) decreases. This is not a marketing trick—it’s a physical limit of the compressor pump and motor. A Chicago Pneumatic CPS 1600-150 delivers 1600 CFM at 100 PSI but only 1450 CFM at 150 PSI. Matching a tool requires checking its CFM demand at your working PSI, not the compressor’s maximum advertised flow.
That drop in airflow under higher pressure is where most tool failures start. You buy a compressor rated for 10 CFM at 90 PSI, then run a sandblaster that needs 12 CFM at that same pressure. The compressor never catches up. The motor overheats trying to maintain a pressure it can’t physically supply with enough volume. It seizes within a month.
What follows is how to read any manufacturer’s chart, why tank size is a separate conversation from CFM, and the one field calculation that prevents buying the wrong machine for your shop.
Key Takeaways
- CFM drops as PSI rises. Never shop by the CFM number at the lowest pressure. Find the CFM at your tool’s required working PSI.
- Tank size is a buffer, not a source. A large tank gives you a longer run time before the pump kicks on, but it doesn’t increase the pump’s maximum CFM output.
- Match sustained CFM, not peak. Your compressor’s duty cycle (e.g., 50%, 75%) tells you the CFM it can deliver continuously without overheating. Ignoring it burns out the motor.
- Add a 30% buffer. If your most demanding tool needs 10 CFM, look for a compressor that can deliver at least 13 CFM at the same PSI. This accounts for line loss, fittings, and future tools.
- Electric motors need correct voltage. A 5 HP compressor on a 120V circuit will never reach its rated CFM; it needs 240V. Check your shop’s electrical capacity first.
How Pressure Changes Flow (The CFM vs PSI Trade-Off)
The relationship is mechanical, not optional. The compressor’s pump and motor have a fixed power input. To compress air to a higher pressure, the pump must work harder against greater resistance. This leaves less available power to move a high volume of air. Think of blowing up a balloon. It’s easy to move a lot of air quickly when the balloon is empty (low pressure). As it fills and pressure rises, you can only push smaller, slower puffs of air (lower volume) to keep going.
Manufacturer spec sheets prove this. Look at the Chicago Pneumatic CPS 400E electric portable compressor.
| Working Pressure (PSI) | Free Air Delivery – FAD (CFM) |
|---|---|
| 58 | 416 |
| 100 | 406 |
| 125 | 403 |
| 150 | 403 |
The CFM drops as the PSI climbs. The difference between 58 PSI and 150 PSI is 13 CFM. That’s enough air to run a small die grinder. If you bought this compressor expecting 416 CFM for a tool that operates at 150 PSI, you’d be short from the first trigger pull.
The published performance data for the Chicago Pneumatic CPS 400E shows a Free Air Delivery of 416 cubic feet per minute at 58 pounds per square inch. At its maximum working pressure of 150 PSI, the delivered airflow falls to 403 CFM, illustrating the inherent trade-off between system pressure and volumetric flow rate in a fixed-speed rotary screw compressor.
This is why the phrase “CFM at PSI” is the only honest spec. A compressor advertised as “10 CFM!” is meaningless. You must ask, “10 CFM at what PSI?” For tools like sandblasters or large die grinders that need high pressure and high volume, this trade-off dictates your entire compressor class.
Decoding the Chart: SCFM, CFM, and What You Actually Get
You’ll see three terms: SCFM, CFM, and FAD. They are not the same, and the difference costs you real air.
- SCFM (Standard Cubic Feet per Minute): This is a theoretical volume measured at a “standard” atmospheric condition (68°F, 36% relative humidity, at sea level). It’s useful for comparing compressors in a lab. It’s almost always a higher, prettier number than what the machine will do in your 95°F garage.
- CFM (Cubic Feet per Minute): A more general term for airflow. In marketing, it’s often used interchangeably with SCFM, which creates confusion.
- FAD (Free Air Delivery): This is the gold standard. It’s the actual, measured volume of air the compressor delivers at its outlet, stated at the working pressure you choose. It accounts for all internal losses. This is the number on a real performance chart. When you see FAD on a spec sheet from Atlas Copco or Chicago Pneumatic, that’s the air you can plan your shop around.
Where this goes sideways: Buying by SCFM alone. A compressor rated for 5.2 SCFM at 90 PSI might only deliver 4.1 CFM (FAD) under the same conditions in your workshop. Your 5 CFM tool will stall, and you’ll blame the tool.
The fix is to ignore the SCFM vs CFM debate on the sticker and look for the FAD chart in the manual or technical datasheet. If a manufacturer doesn’t publish a pressure/flow chart, be suspicious. Reputable brands like Kaeser and CompAir provide these charts for every model. For the DIYer, understanding the difference between SCFM and CFM is the first step to cutting through the marketing.
The Tools Dictate the Rules (A Real Matching Table)
Your compressor’s job is to feed your tools. The tool’s air consumption rating is non-negotiable. This rating is always given as CFM at a specific PSI. You must meet or exceed both numbers.
Here’s a concrete look at common tool demands versus what different compressor classes actually deliver.
| Tool / Application | Typical PSI Requirement | Typical CFM Demand | Compressor Class Required |
|---|---|---|---|
| Brad Nailer | 70-100 PSI | 0.3 – 0.5 CFM | Small Portable (1-3 HP) |
| Framing Nailer | 70-120 PSI | 2.0 – 2.5 CFM | Small Portable (3-5 HP) |
| Die Grinder | 70-90 PSI | 4.0 – 8.0 CFM | Large Portable / Stationary (5+ HP) |
| 1/2″ Impact Wrench | 90 PSI | 4.0 – 5.0 CFM | Large Portable (5-6 HP) |
| Small Sandblaster | 90-100 PSI | 8.0 – 12.0 CFM | Stationary (7.5+ HP) |
| Large Sandblaster | 100+ PSI | 15.0 – 20.0 CFM | Industrial (10+ HP, Two-Stage) |
See the jump for sandblasting? A typical 5 HP “big box” compressor might advertise 15 CFM—but that’s at 40 PSI. At 100 PSI, its FAD might be 9 CFM. It cannot run a small sandblaster. This mismatch is the most common cause of compressor failure in auto shops.
The solution is a two-step check. First, find your tool’s true CFM at its operating PSI. Second, verify your compressor’s FAD at that same PSI exceeds the tool’s demand. Our guide on determining compressor needs walks through this math.
Duty Cycle: The Hidden Governor on Your CFM
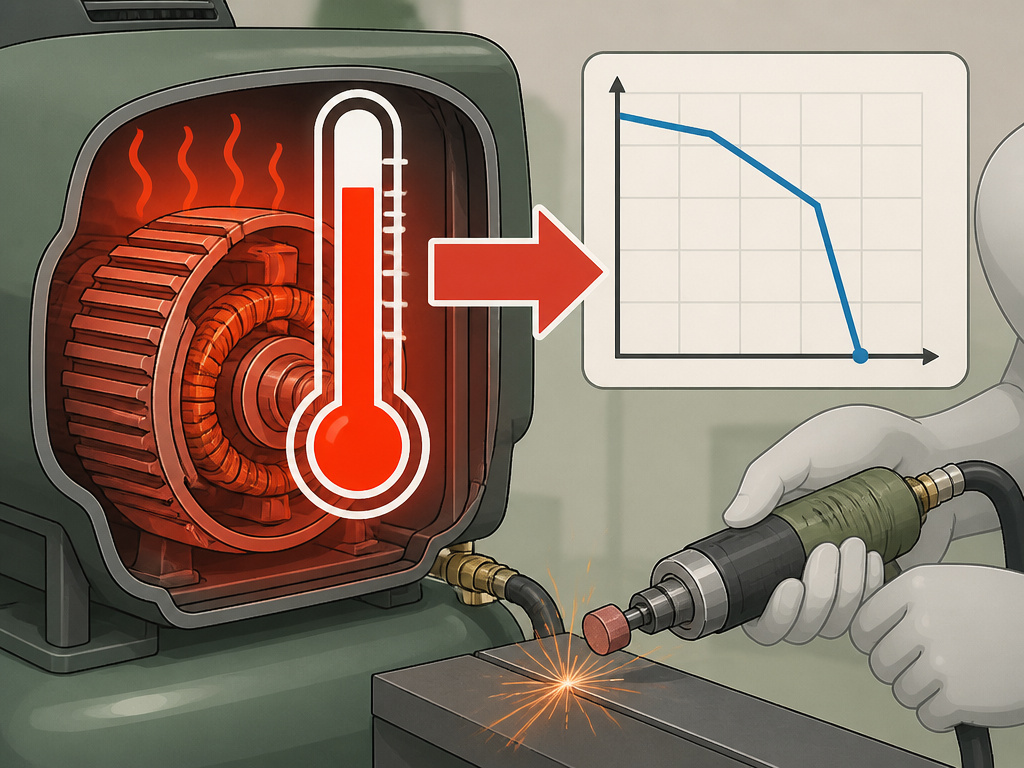
A compressor’s duty cycle is the percentage of a 10-minute cycle it can run without overheating. A 50% duty cycle means it can run for 5 minutes, then must cool for 5 minutes. This rating directly caps your sustained CFM.
- Pancake/Small Portables (100% Duty Cycle): These are designed for intermittent use like nailers. They can run until the tank is full, stop, and restart. Their CFM is low.
- Large Portables (50-75% Duty Cycle): These have more power but generate more heat. Running a die grinder continuously for 10 minutes on a 50% duty cycle compressor will trip its thermal overload.
- Industrial Stationary (100% Duty Cycle): These are built for continuous operation with enhanced cooling. The CFM rating is what you get, all day.
Common mistake: Using a 50% duty cycle compressor for a continuous-application tool like a sandblaster or sander. The compressor will thermal shutoff every 10-15 minutes, drastically slowing your work and stressing the motor to an early death.
If you need sustained air, the duty cycle is more important than peak horsepower. A 5 HP compressor with a 100% duty cycle is a vastly different machine from a 5 HP compressor with a 50% duty cycle. The first is for a production shop; the second is for a home garage. Always check the spec sheet or nameplate.
Tank Size vs. CFM: The Reservoir Myth

This confusion loses people more money than any other spec. The tank is an air reservoir. The pump (which determines CFM) is the well that fills it.
- Large Tank, Small Pump: You get a long, strong initial blast of air as the tank empties. Then you wait a long time for the small pump to refill the tank. Good for short, high-demand tasks with long breaks in between (like running an impact wrench to remove lug nuts).
- Small Tank, Large Pump: The tank empties quickly, but the powerful pump refills it almost immediately. This provides a more consistent, steady airflow for continuous-use tools (like a die grinder or sander).
The tank does not increase your compressor’s CFM. A 20-gallon tank and a 60-gallon tank on the same pump will deliver the same CFM to your tool. The 60-gallon tank just lets you run longer before the pump kicks on. For continuous tools, you need a high-CFM pump first, and a large tank second. Our article on the best compressor for air tools breaks this down by tool type.
Putting It Together: A Step-by-Step Buying Method
Forget the chart for a minute. Follow this sequence.
- List Your Tools: Write down the two numbers for your most air-hungry tool: its required PSI and its CFM consumption at that pressure.
- Find Real FAD: Look at compressor spec sheets. Ignore all “SCFM” or “CFM” headlines. Find the technical data table with “Free Air Delivery (FAD) at X PSI.” This is your true supply number.
- Apply the Buffer: Multiply your tool’s CFM demand by 1.3. This is your target compressor FAD. This covers air leaks, hose friction, and future tool purchases.
- Check the Duty Cycle: If you’ll use the tool continuously for more than a few minutes, ensure the compressor’s duty cycle is 75-100%. For intermittent use, 50% is acceptable.
- Verify Electrical Needs: A true 5+ HP compressor requires a 240V circuit. Confirm your shop’s wiring before you buy.
This method turns abstract chart reading into a actionable checklist. If you need to calculate CFM requirements for a custom setup, the same principles apply.
Frequently Asked Questions
Why does my compressor’s CFM drop when I add a second tool?
You’re exceeding the pump’s capacity. Each tool consumes a portion of the total CFM the compressor can produce. If Tool A uses 5 CFM and Tool B uses 4 CFM, but your compressor only delivers 8 CFM at that pressure, the system pressure will fall. Both tools will stall or run weakly. The compressor motor will also overwork trying to meet the demand.
Is a 200 PSI compressor always better than a 150 PSI model?
Only if your tools require that pressure. A 200 PSI compressor like some Atlas Copco mobile units is built for industrial drilling or sandblasting. For the same horsepower, a compressor designed for 200 PSI will often have a lower CFM at 100 PSI than a model designed for 150 PSI. You pay for pressure capability you don’t use, sacrificing airflow. Buy the pressure you need, then maximize CFM at that point.
Can I increase my compressor’s CFM?
You cannot increase the pump’s fundamental mechanical CFM output. However, you can improve the effective delivery to your tool. Ensuring proper pressure adjustment for efficiency, using larger diameter hoses (3/8″ instead of 1/4″), shortening hose length, and eliminating leaks all help more of the compressor’s rated CFM reach your tool. For systemic upgrades, we cover ways to increase CFM on an existing system.
What’s more important for painting: high CFM or high PSI?
Consistent, clean, and dry air is most important. A typical HVLP spray gun needs only 7-12 CFM at 40-50 PSI. The critical factor is having a compressor with enough CFM to supply that air continuously (a high duty cycle) and pairing it with effective filters and dryers to remove oil and moisture. A large tank is also beneficial to prevent the pump from cycling and introducing pressure fluctuations during a pass.
The Bottom Line
Reading an air compressor CFM vs PSI chart isn’t about comparing columns. It’s about seeing the single performance curve of a machine. Your job is to place your tool’s needs on that curve and see if the machine lives above it.
Stop looking at the biggest number on the tag. Find the Free Air Delivery (FAD) at your working pressure. Respect the duty cycle. Understand that the tank is just a battery, not the engine. When you match the real, sustained CFM to the job, the compressor becomes a silent partner. When you miss by even 10%, it becomes the loudest, most expensive problem in your shop.
